


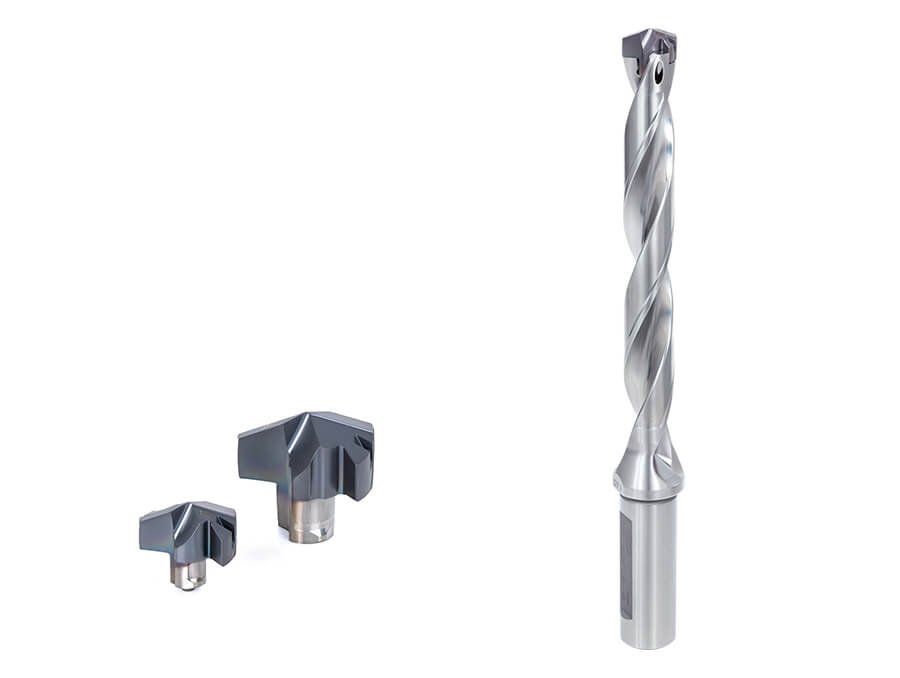
DrillMeister -Spacer part- DMH head eliminated chipping issues

IMPROVED TOOL LIFE AND PRODUCTIVITY
In this application, edge chipping caused by shallow through-hole drilling and low machine rigidity was the main challenge.
By applying the high-edge-strength DMH head, stable machining was achieved while increasing cutting speed by approximately 20%.
Tool life improved from 4,000 holes to 8,000 holes, doubling the service life and delivering both higher productivity and longer tool life.
Share
| Industry | Engineering |
|---|---|
| Component | Spacer |
| Material ISO code |
 P - Steel |
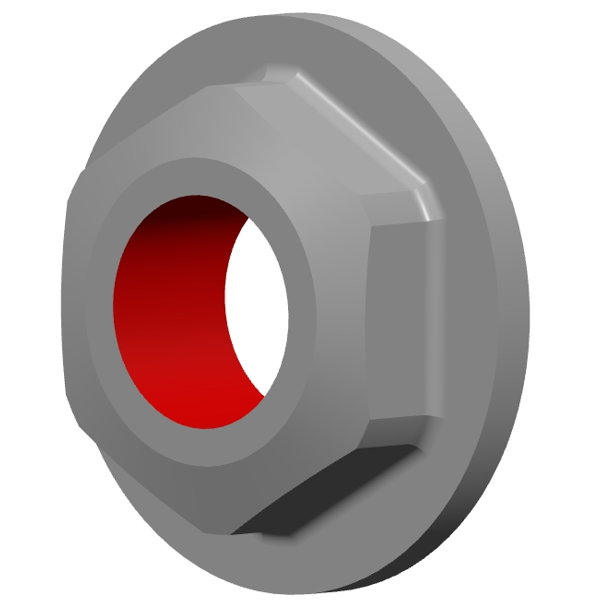
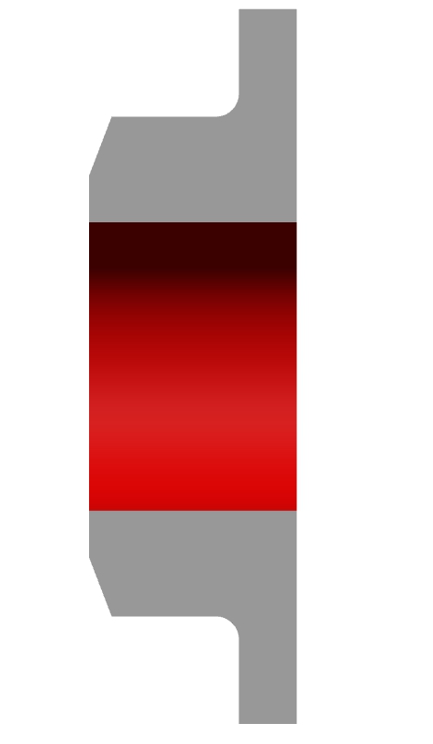
| Work material | SCr435H/37Cr4/5135H |
| Machine(spindle type) | CNC Lathe |
| Tool family | Holemaking |
| Tool category | Drilling |
| Product name | DrillMeister |
| TSR No. | 5688H |
Tool
| Tungaloy | Competitor | |
|---|---|---|
| Body | TID125F16-3 | Head exchangable drill 3xD |
| Head | DMH125 | Drill head 12.5mm |
| Grade | AH9130 | PVD |
Tool life
| Tungaloy | Competitor | |
|---|---|---|
| Tool life (m/insert) | 72 | 36 |
| Number of workpieces (pcs/insert) | 72000 | 36000 |
Cutting conditions
| Tungaloy | Competitor | |
|---|---|---|
| Tool diameter DC (mm) | 12.5 | 12.5 |
| Hole tolerance grade | IT10 | IT10 |
| Surface quality required Ra (μm) | Good | Good |
| Cutting speed V/c (m/min) | 98 | 82 |
| Feed f (mm/rev) | 0.25 | 0.25 |
| Feed speed Vf (mm/min) | 2496 | 2088 |
| Coolant | Internal coolant | Internal coolant |