


TungMeister – Shaft – AH715

IMPROVED PRODUCTIVITY AND TOOL LIFE
The customer previously machined the keyway in two operations: pre-drilling with a ø8 drill followed by slotting with a ø8 end mill.
By adopting the TungMeister VVFH head, which is capable of drilling, the process was consolidated into a single operation. After optimizing the feed per tooth to the recommended fz = 0.03 mm/t, tool life improved from 126 components with the competitor's tool to 160 components. Chip removal rate also increased from 3.82 cm³/min to 8.59 cm³/min, achieving both process consolidation and extended tool life.
Share
| Industry | Automotive |
|---|---|
| Component | Shaft |
| Material ISO code |
 P - Steel |
| Work material | S45C/C45 |
| Machine(spindle type) | Multi-Tasking Machine |
| Tool family | Milling |
| Tool category | Slot milling |
| Product name | TungMeister |
| TSR No. | 5674M |
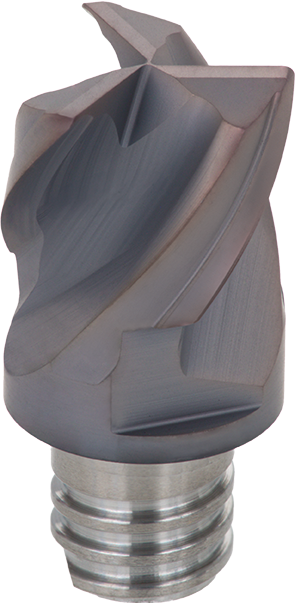
Tool
| Tungaloy | Competitor | |
|---|---|---|
| Body | VSSD10L055S05-S | φ8 Solid Endmill |
| Number of teeth | 3 | 4 |
| Cutting diameter | 8 | 8 |
| Insert | VVFH0800S03R04S05 | |
| Number of cutting edges | 1 | 1 |
| Grade | AH715 | PVD |
Cutting conditions
| Tungaloy | Competitor | |
|---|---|---|
| Cutting speed V/c (m/min) | 60 | 60 |
| Feed per tooth f/z (mm/t) | 0.03 | 0.01 |
| Feed f (mm/rev) | 0.09 | 0.04 |
| Feed speed Vf (mm/min) | 215 | 95 |
| Depth of cut ap (mm) | 5 | 5 |
| Width of cut ae (mm) | 8 | 8 |
| Coolant | Exteranal | Exteranal |