


TungMeister – Shaft – AH715

IMPROVED PRODUCTIVITY AND TOOL CONSOLIDATION
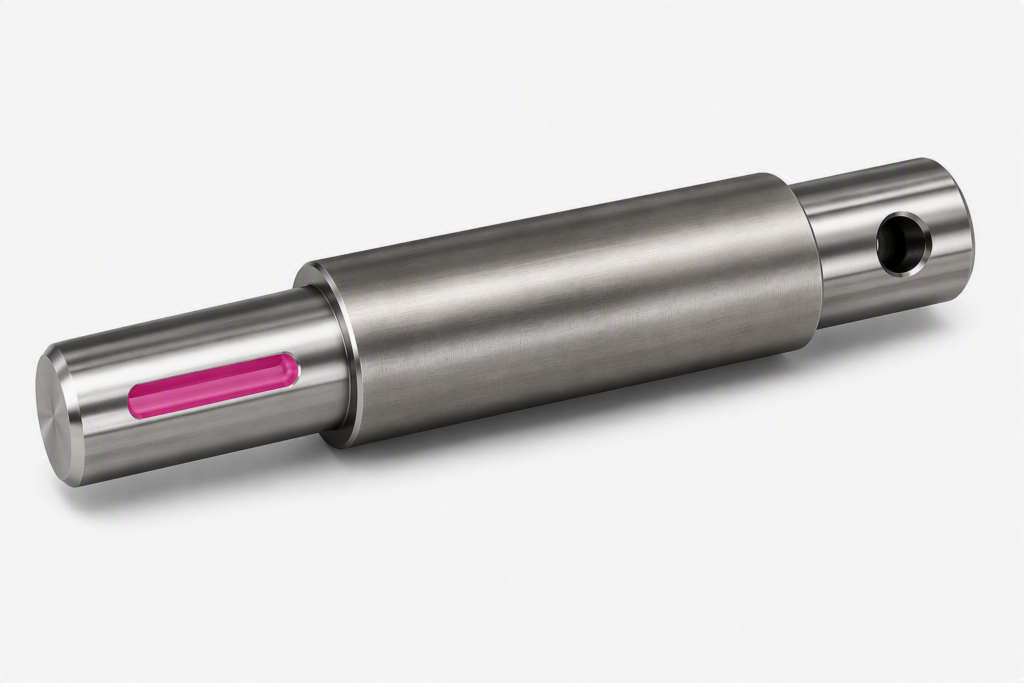
The customer previously machined the keyway in three operations: pre-drilling with a flat drill, rough slotting with a roughing end mill, and finishing with a finishing end mill.
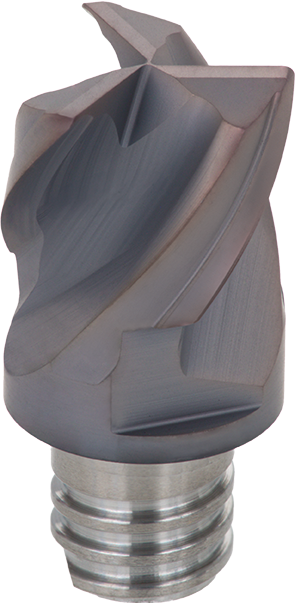
By adopting the TungMeister VVFH head, which is capable of drilling, the pre-drilling and roughing operations were consolidated, reducing the process to two operations — roughing and finishing. The number of tools required was also reduced from three to one. With the overhang shortened from 20 mm to 15 mm and the feed per tooth set at fz = 0.07 mm/t, surface finish quality was improved as well, achieving both process consolidation and enhanced machining quality.
Share
| Industry | Automotive |
|---|---|
| Component | Shaft |
| Material ISO code |
 P - Steel |
| Work material | SCM420 |
| Machine(spindle type) | Multi-Tasking Machine |
| Tool family | Milling |
| Tool category | Slot milling |
| Product name | TungMeister |
| TSR No. | 5675M |
Tool
| Tungaloy | Competitor | |
|---|---|---|
| Body | VSSD12L065S06-S | φ9 Solid Roughing EndMill |
| Number of teeth | 3 | 4 |
| Cutting diameter | 10 | 9 |
| Overhang (mm) | 15 | 20 |
| Insert | VVFH1000S03R04S06 | |
| Number of cutting edges | 1 | 1 |
| Grade | AH715 | PVD |
Cutting conditions
| Tungaloy | Competitor | |
|---|---|---|
| Cutting speed V/c (m/min) | 100 | 100 |
| Feed per tooth f/z (mm/t) | 0.07 | 0.05 |
| Feed f (mm/rev) | 0.21 | 0.2 |
| Feed speed Vf (mm/min) | 668 | 707 |
| Depth of cut ap (mm) | 3.5 | 3.5 |
| Width of cut ae (mm) | 10 | 9 |
| Coolant | Dry | Dry |