


DeepTriDrill – AISI/SAE 1045 H – AH725

35% faster cycle times and superior surface finish in hydraulic cylinder manufacturing
Drilling Ø32 mm × 600 mm deep holes in AISI/SAE 1045 H (230 HB) with conventional tools means drilling from both sides — poor finish, misalignment, and frequent insert changes.
DeepTriDrill with AH725 grade solves this in a single pass.
10× tool life — 20 holes per edge vs. 2
35% faster — 215 mm/min at 120 mm/min
Single-pass H8 tolerance — no secondary finishing operations.
3-edge insert — extermely lower cost per cutting edge
Share
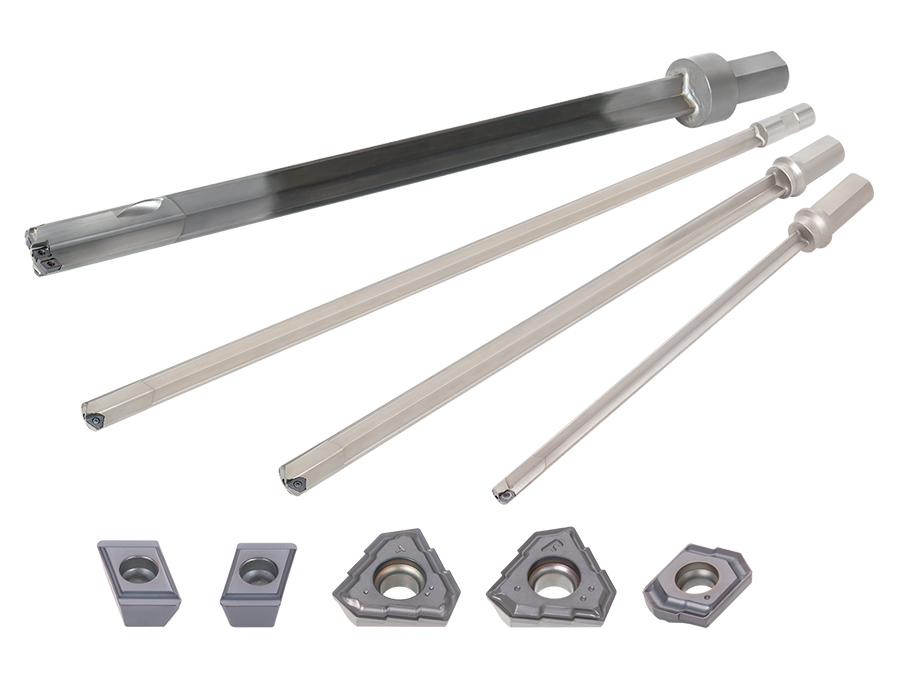
| Industry | Engineering |
|---|---|
| Component | Bar |
| Material ISO code |
 P - Steel |
| Work material | AISI/SAE 1045 H |
| Material hardness | 230HB |
| Machine(spindle type) | Multi-Axis Machining Center |
| Tool family | Holemaking |
| Tool category | Deep hole drilling |
| Product name | DeepTri-Drill |
| TSR No. | 5201D |
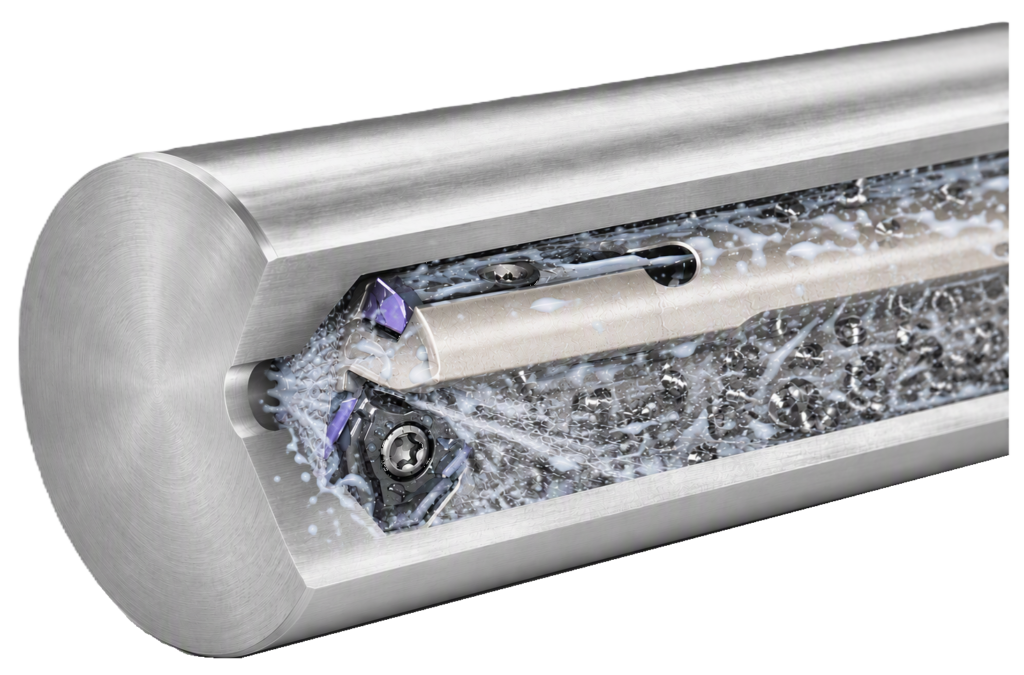
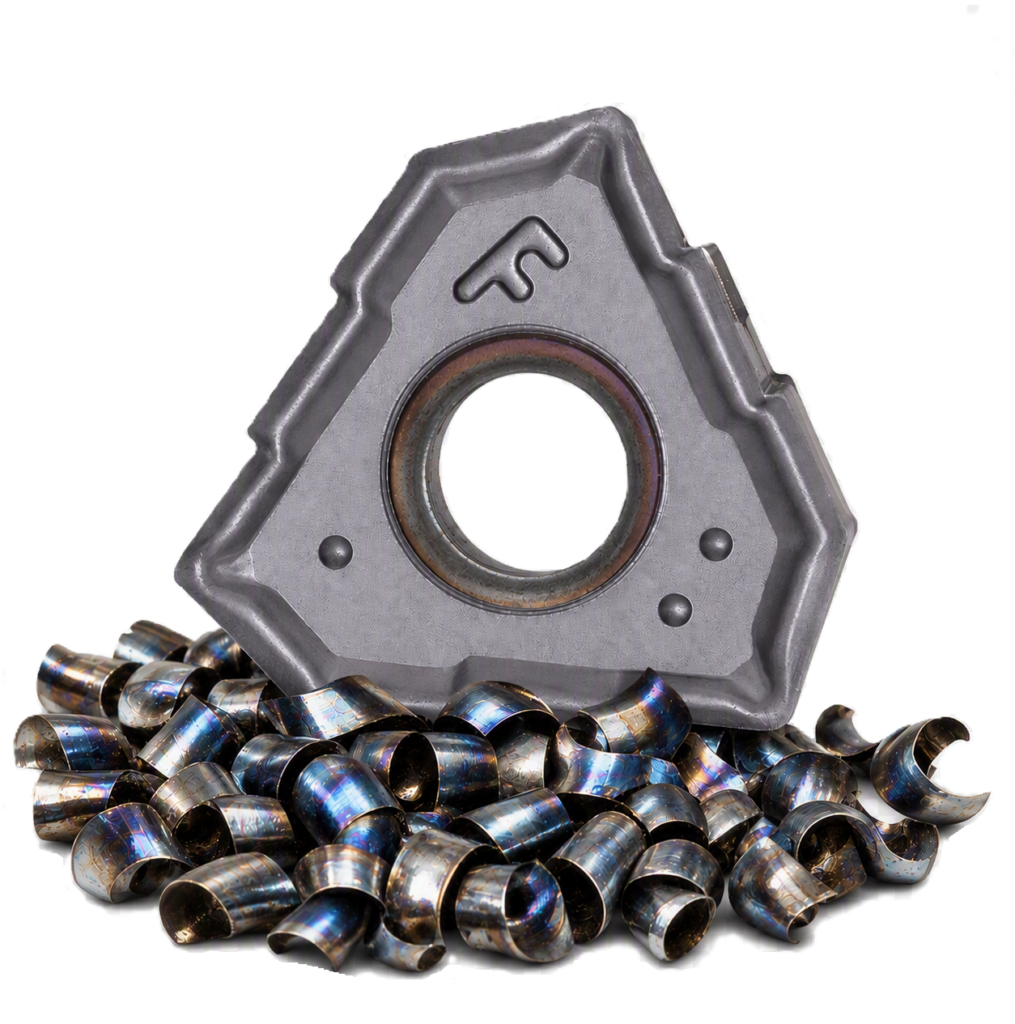
Tool
| Tungaloy | Competitor | |
|---|---|---|
| Body | TRLG32.00X1000-M40 | indexable drill K |
| Insert | TOHT130408-DT AH725 | indexable insert |
| Grade | AH725 | coated carbide insert |
Tool life
| Tungaloy | Competitor | |
|---|---|---|
| Tool life (m/insert) | 36 | 1.2 |
| Number of workpieces (pcs/insert) | 60 | 2 |
Cutting conditions
| Tungaloy | Competitor | |
|---|---|---|
| Tool diameter DC (mm) | 32.00 | 32.00 |
| Hole tolerance grade | H8 | H8 |
| Hole depth H (mm) | 600 | 600 |
| Cutting speed V/c (m/min) | 120 | 100 |
| Feed f (mm/rev) | 0.18 | 0.16 |
| Feed speed Vf (mm/min) | 215 | 159 |