


DrillMeister TungFlex connection – Pump rotor-

IMPROVED TOOL LIFE
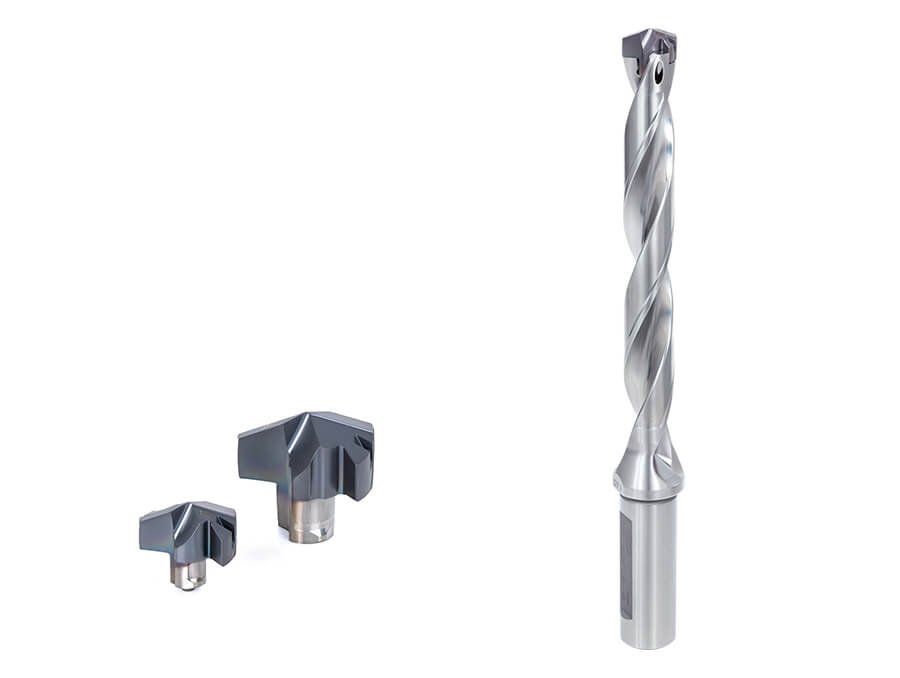
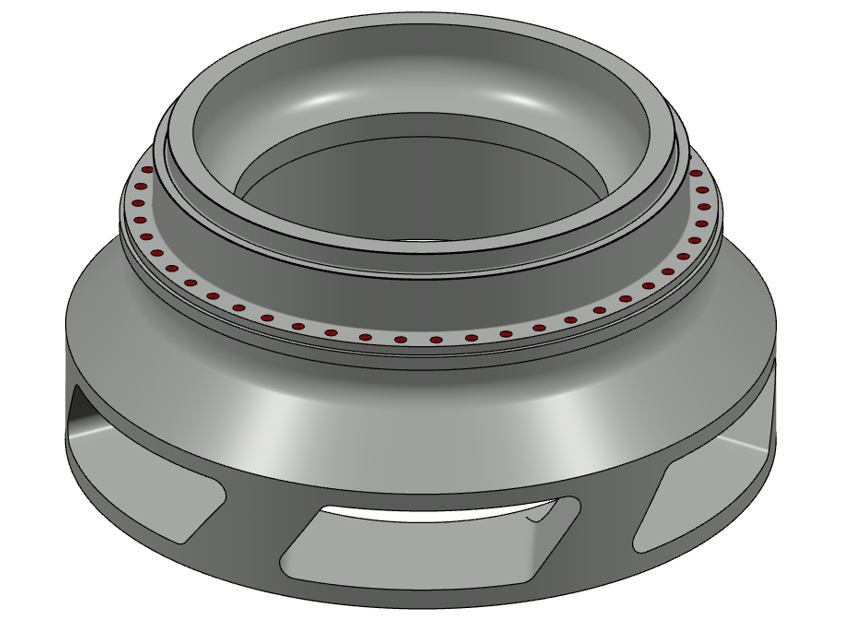
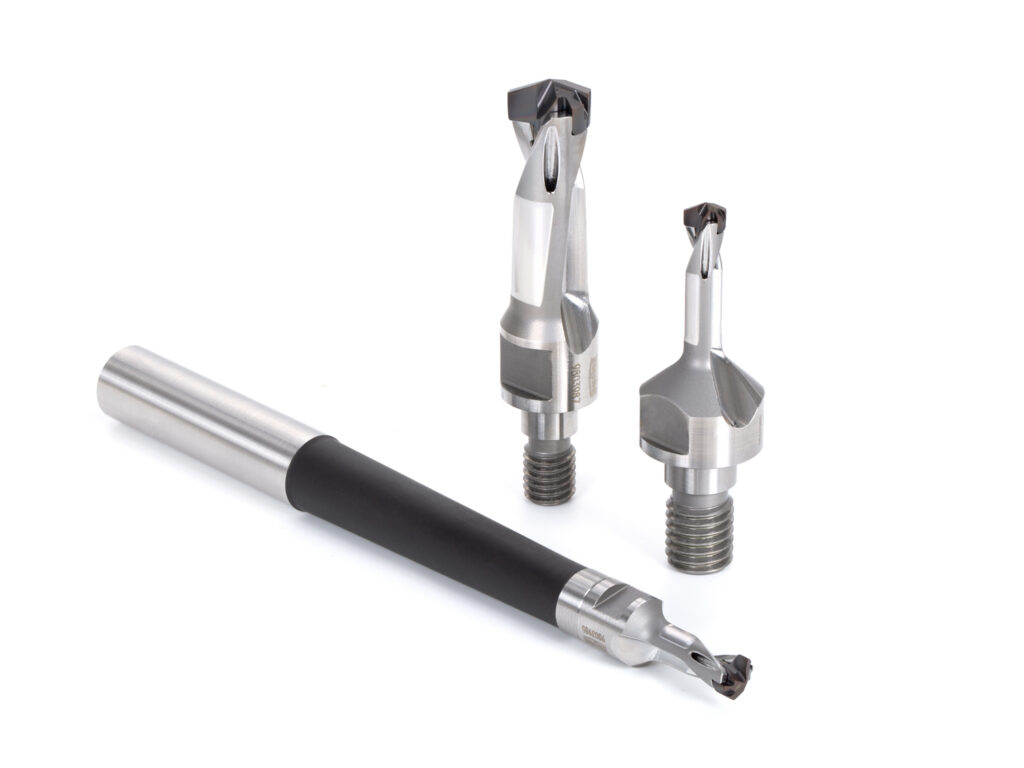
In this application, an 8×D tool overhang was required to avoid interference, while the actual hole depth was less than 3×D. The existing competitor's 8×D drill suffered from unstable machining due to the long overhang condition, resulting in cutting edge chipping and limited tool life. To address this issue, the DrillMeister modular shank was selected to provide a highly rigid tooling setup capable of maintaining stability even under extended overhang conditions. As a result, excellent machining stability was achieved, edge chipping was effectively suppressed, and tool life was improved approximately threefold, increasing from 324 holes to 972 holes.
Share
| Industry | Oil & Gas |
|---|---|
| Component | Pump roter |
| Material ISO code |
 P - Steel |
| Work material | C35 |
| Machine(spindle type) | Machining Center Large(#50,HSK100) |
| Tool family | Holemaking |
| Tool category | Drilling |
| Product name | DrillMeister |
| TSR No. | 5687H |
Tool
| Tungaloy | Competitor | |
|---|---|---|
| Body | TID170M12-3 | Head exchangable drill 8xD |
| Head | DMP175 | Drill head 17.5mm |
| Grade | AH9130 | PVD |
Tool life
| Tungaloy | Competitor | |
|---|---|---|
| Tool life (m/insert) | 43.7 | 14.6 |
Cutting conditions
| Tungaloy | Competitor | |
|---|---|---|
| Tool diameter DC (mm) | 17.5 | 17.5 |
| Hole tolerance grade | ±0.1 | ± |
| Surface quality required Ra (μm) | Good | Good |
| Hole depth H (mm) | 45 | 45 |
| Cutting speed V/c (m/min) | 82 | 82 |
| Feed f (mm/rev) | 0.35 | 0.35 |
| Feed speed Vf (mm/min) | 522 | 522 |
| Coolant | Internal coolant | Internal coolant |